


2026 manufacturer qualification guide | Trauma locking plate systems
The right trauma locking plates manufacturer must prove control of the entire plate-screw-instrument system: product definition, implant material, locking interfaces, machining, finishing, cleanliness, verification, market authorization, set availability and lifecycle support. This guide converts those requirements into a practical distributor scorecard.
How Should You Choose a Trauma Locking Plates Manufacturer?
Choose the manufacturer that can provide verified evidence for the exact plate families, screw interfaces, instruments, destination markets and supply model you require. Begin with legal-manufacturer identity and product authorization, then examine engineering controls, materials, manufacturing, inspection, verification and validation, packaging, delivery performance, complaints and change notification.
Shortlist two or three suppliers using the same request-for-information package. Audit the highest-risk processes, approve representative samples and complete a controlled first production lot before scaling the catalog. Do not qualify a factory only from catalog breadth, certificate images, equipment photographs or a low quotation.
Best short answer: a qualified locking plate manufacturer can repeatedly make the approved plate-screw-instrument system and can prove it with current, product-linked and market-specific evidence.
What a Locking Plate Manufacturer Must Prove
This page is the broad manufacturer-selection guide. For one product-family example, see the separate distal tibiofibular locking plate OEM manufacturing guide. Keeping the pages at different levels avoids keyword cannibalization: this page targets manufacturer qualification, while the supporting page targets a specific plate manufacturing program.
1Portfolio and Plate-System Fit
Start with the distributor's procedure and inventory map. Define anatomical regions, plate types, left/right variants, lengths, hole counts, compatible screws, instrument sets, sterile or non-sterile supply and target countries. A large catalog is useful only when the exact devices are authorized, documented and supportable in the intended market.
Distinguish fixed-angle locking holes, polyaxial or variable-angle mechanisms, combination holes and non-locking options. These terms do not establish performance by themselves. Each design needs its own compatibility, insertion, verification and labeling evidence.
Review XC Medico's current trauma implant and locking plate portfolio and locking plate product families, then request a controlled model and compatibility list for the proposed contract.
2Implant Materials and Lot Traceability
Specify the governing material standard, grade, product form, condition and project requirements. ASTM F136, for example, covers wrought annealed Ti-6Al-4V ELI alloy for surgical implant applications. Generic terms such as "medical titanium," "Grade 5," "Grade 23" or "TC4" should not replace the approved material specification.
Alternative titanium alloys, commercially pure titanium or stainless steel may be appropriate for particular devices when supported by the design and regulatory dossier. The buyer should not impose a material solely because it appears in another manufacturer's system.
Run a trace exercise from one finished plate and screw back to raw-material heat or lot, receiving acceptance, manufacturing traveler, outsourced processing, inspection, cleaning, labeling, packaging and release. Review the published XC Medico orthopedic quality-control process, but qualify the exact products with actual records.
3Locking Interfaces, Screws and Instruments
The locking mechanism is the defining interface of the system. Review locking-hole geometry, screw-head geometry, trajectories, insertion range where applicable, thread or engagement features, driver connection, drill guide and insertion technique. Control how compatible components are identified and prevent mixing with visually similar but incompatible parts.
Variable-angle systems add manufacturing and inspection complexity. Require the approved angular range, insertion technique, compatible screws and guides, interface acceptance criteria and evidence supporting the marketed design. Do not accept a universal angle claim copied across unrelated plate families.
Buyers who need a commercial-team primer can read the separate explanation of locking versus non-locking plates; final product and clinical decisions remain subject to the applicable labeling and professional judgment.
4Manufacturing Capability and Metrology
Map each selected plate through machining, forming where applicable, heat treatment, finishing, anodizing or other surface processing, cleaning, marking, packaging and sterilization where applicable. Identify which activities occur at the certified site and which are outsourced.
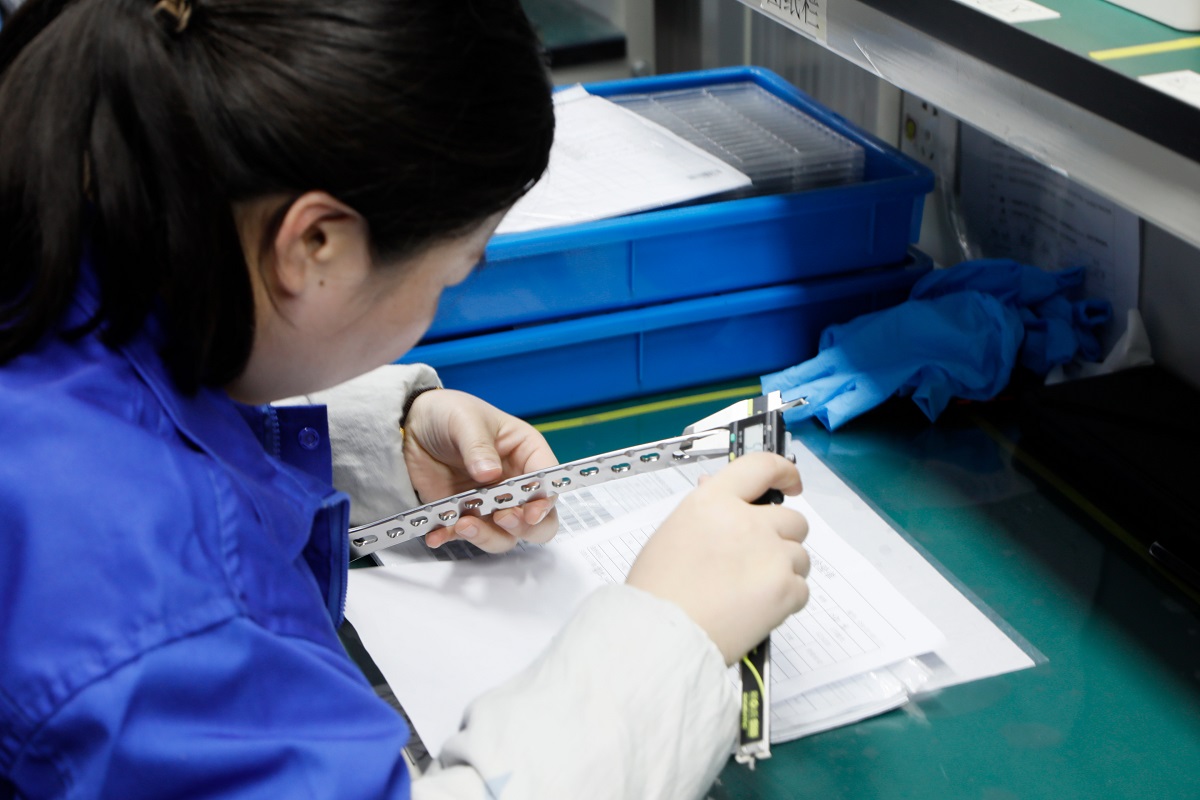
CNC equipment supports complex production, but machine count and brand do not demonstrate capability. Examine controlled programs, fixtures, setup approval, tool-life rules, maintenance, calibrated inspection equipment, measurement-system suitability, sampling plans, nonconformance and rework.
Visit the published orthopedic implant workshop and orthopedic product manufacturing process, then verify the proposed routing and records during a remote or on-site audit.
5Surface Condition, Cleanliness and Packaging
Surface processes should have controlled inputs, parameters and acceptance criteria. Define requirements for burrs, edges, scratches, pits, embedded media, color variation and other relevant conditions. Anodizing or color coding must not be treated as decoration only; verify process control, product identification and any required performance evidence.
ISO 19227:2018 specifies general cleanliness requirements and test methods for validation and control based on risk management. It does not prescribe one universal test panel or acceptance limit for every implant. Ask the manufacturer to identify process residues and justify the methods, limits and sampling used for the specific product family.
If the product is supplied sterile, validate the chosen sterilization method, sterile barrier, forming and sealing, distribution performance and shelf life. If non-sterile, define protective packaging, cleanliness, labeling and reprocessing responsibilities. ISO 11607 addresses packaging systems for terminally sterilized medical devices but does not itself prove that one blister configuration is suitable.
6Verification, Mechanical Testing and Worst-Case Rationale
Testing must follow the device design, intended use, risk analysis and regulatory pathway. ASTM F382 is widely referenced for metallic bone plates, but its exact use and the suitability of a test configuration must be determined for the subject plate. Do not demand a generic F382 report and assume that it covers every anatomical or complex plate.
The FDA's November 2024 guidance for orthopedic non-spinal bone plates, screws and washers describes current recommendations for device information and performance testing in 510(k) submissions. A separate FDA guidance provides performance criteria for fracture fixation plates within the Safety and Performance Based Pathway. Confirm whether the subject device falls within the stated scope.
Worst-case selection should consider geometry, material, size, thickness, holes, working length, interfaces and the chosen test method. Require an engineering rationale that maps each plate family to representative test articles. Reports must identify the tested model, drawing revision, material lot, production process, method, acceptance criteria, deviations and conclusion.
7QMS, Product Authorization and Post-Market Readiness
Verify the ISO 13485 certificate's organization, address, scope, issuing certification body, accreditation, status and expiry. The certificate supports quality-system evaluation but does not authorize every product in the catalog.
- United States: FDA guidance identifies in-scope non-spinal, non-resorbable bone plates and screws as Class II devices. Determine the exact classification, product code and applicable premarket route. A 510(k) is device-specific, not a factory certification. The FDA Quality Management System Regulation became effective February 2, 2026.
- European Union: confirm classification under MDR Annex VIII for the exact device. Long-term surgically invasive and implantable devices generally enter Rule 8, but exceptions and device characteristics can change the result. Verify the legal manufacturer, Notified Body scope where applicable, certificate, Declaration of Conformity, UDI/device data and economic operators.
- Other markets: create a country-by-country matrix for registration owner, documents, testing, labels, languages, local representation, vigilance and renewal. Do not use a generic "LATAM dossier" as a substitute for national requirements.
Post-market controls should define complaint intake, adverse-event escalation, investigations, CAPA, trend review, recalls or field safety actions, returned-product handling and change notification. Review XC Medico's published after-sales and complaint support, then assign responsibilities in a written agreement.
A Controlled OEM/ODM Partnership Workflow
OEM/ODM can range from private-label packaging of an authorized standard product to a new plate design. Define the scope before discussing timeline or price. New geometry or interfaces can trigger design-control, verification, validation and regulatory work that a label change does not.
XC Medico's current orthopedic OEM/ODM service page describes support from engineering through production. Buyers should convert published capabilities into product-specific deliverables, owners, dates and acceptance criteria.
Low MOQ and sample programs
A low MOQ can reduce initial inventory risk, but it is a commercial term, not quality evidence. Define engineering samples, verification or validation units, the initial commercial quantity per SKU and routine replenishment MOQ separately. Confirm whether "one set" means one plate set, one complete instrument set, one side, one size matrix or a mixed system.
Supply chain and inventory evidence
Do not promise Mexico hubs, next-day delivery or specific fill rates without a signed logistics model and measured performance. Ask for lead time by product family, normal and peak capacity, stocked SKUs, order-confirmation timing, minimum order quantities, OTIF or fill-rate definitions, recent performance, shortage escalation and business continuity.
If regional warehousing is proposed, verify facility address, regulatory role, stocked products, inventory ownership, environmental requirements, traceability, FEFO where applicable, returns, recalls and service levels. Compare those records with XC Medico's published supply-chain and warehousing model.
100-Point Trauma Locking Plate Manufacturer Scorecard
Score each category from 0 to 5 and multiply it by the weighting. Keep the evidence reviewed beside every score. Mandatory gates must pass even when the weighted total is high.
| Criterion | Weight | Core evidence | Mandatory gate? |
|---|---|---|---|
| 1. Portfolio and plate-system fit | 10% | Authorized model matrix, plate-screw-instrument compatibility and destination-market availability. | For scope |
| 2. Materials and traceability | 15% | Approved specifications, mill certificates, heat/lot trace and receiving controls. | Yes |
| 3. Locking interfaces and instruments | 15% | Controlled drawings, compatibility, functional evidence, guides, drivers and set records. | Yes |
| 4. Manufacturing and metrology | 15% | Process/site map, validation, calibrated measurement, capability and nonconformance controls. | Yes |
| 5. Surface, cleanliness and packaging | 10% | Surface criteria, cleaning evidence, package and sterilization validation as applicable. | Yes for scope |
| 6. Verification and testing | 15% | Risk-linked matrix, worst-case rationale, production-equivalent samples and approved reports. | Yes |
| 7. QMS and regulatory readiness | 15% | ISO 13485 scope, product authorization, labels, technical documents and post-market controls. | Yes |
| 8. Supply and commercial support | 5% | Lead time, inventory, OTIF, continuity, MOQ, warranty, instruments and escalation. | Threshold |
A practical rule can require all mandatory gates to pass, no unresolved critical findings, acceptable samples and first-lot results, and a weighted score above the buyer's predefined threshold. Set the threshold according to device and supply risk rather than copying a universal number.
Evidence scoring scale
| Score | Evidence level | Interpretation |
|---|---|---|
| 0 | No evidence | The requirement is not addressed. |
| 1 | Claim only | A sales or marketing statement has no controlled support. |
| 2 | Incomplete | Evidence is outdated, generic, inconsistent or missing critical scope. |
| 3 | Acceptable | Current controlled records reasonably demonstrate the requirement. |
| 4 | Strong | Product-linked records include recent examples, metrics, traceability and responsible owners. |
| 5 | Verified | Evidence is repeatable, independently confirmed where appropriate and supported by effective controls. |
Documents to Request Before Approving Samples
- Legal-manufacturer, manufacturing-site and outsourcing map.
- Current ISO 13485 certificate with scope and accreditation details.
- Product and market authorization matrix by model family.
- Controlled plate, screw and instrument compatibility matrix.
- Approved material specifications and sample mill certificates.
- Finished-device lot-trace example.
- Critical-to-quality feature and inspection matrix.
- Representative CMM or dimensional inspection reports.
- Locking-interface and instrument functional evidence.
- Surface defect and finishing acceptance standard.
- Cleaning validation or verification rationale.
- Worst-case selection and verification matrix.
- Mechanical and other applicable test summaries.
- Packaging and sterilization evidence where applicable.
- Controlled label, IFU and UDI responsibility matrix.
- Lead-time, capacity, stock and delivery evidence.
- Quality agreement, change-notification and complaint workflow.
- Sample-to-production transfer and first-lot approval plan.
Automatic Escalation or Disqualification Red Flags
Related Locking Plate and Supplier Resources
Start a Locking Plate Manufacturer Review
Prepare the target countries, anatomical plate families, screw and instrument requirements, sterile or non-sterile supply condition, annual forecast, private-label scope and required documents. XC Medico can then confirm available systems, OEM/ODM scope, current MOQ, sample plan and estimated lead time.
Frequently Asked Questions
What should a trauma locking plates manufacturer provide?
At minimum, request legal and site identity, current QMS evidence, product authorization by market, controlled plate-screw-instrument compatibility, material and traceability records, manufacturing and inspection evidence, verification reports, packaging or sterilization evidence as applicable, delivery data and written change and complaint responsibilities.
Does ISO 13485 certification mean every locking plate is approved?
No. ISO 13485 certification concerns the scope of a quality management system. Product authorization must be verified separately for the exact device, legal manufacturer, manufacturing site, intended use and destination market.
Is ASTM F382 required for every locking plate?
ASTM F382 is a widely referenced specification and test method for metallic bone plates, but applicability and test configuration depend on the device design, regulatory pathway and testing rationale. Complex anatomical designs may require additional or different evaluation. Confirm the current standard revision and applicable authority expectations.
What is the difference between a fixed-angle and variable-angle locking plate?
A fixed-angle system controls the screw trajectory defined by its locking interface. A variable-angle or polyaxial system permits insertion within a specified range using its approved screw and technique. The exact mechanism, range, compatibility and limitations are product-specific and must be verified from controlled documentation.
How do I verify locking screw compatibility?
Review controlled interface drawings and the compatibility matrix, then test production-equivalent plates, screws, guides and drivers using the approved method. Confirm identification, trajectory, engagement, insertion and removal acceptance criteria and controls that prevent component mixing.
Should a manufacturer offer sterile and non-sterile plates?
The required supply condition depends on the product and market strategy. Sterile products need appropriate sterilization, packaging and shelf-life validation. Non-sterile products require controlled cleanliness, protective packaging, labeling and reprocessing responsibilities. A manufacturer does not need to offer both models to be suitable.
How should a distributor compare OEM pricing?
Compare total landed and lifecycle cost: implants, screws, instruments, samples, validation, registration documents, packaging, freight, duties, inventory, replenishment, repairs, replacements, complaints and change management. Ensure every quotation uses the same SKU and service scope.
What is the best way to approve a new locking plate supplier?
Use document prequalification, risk-based audit, representative sample and interface verification, closure of findings, a signed quality agreement and a controlled first production lot. Continue monitoring quality, delivery, complaints, changes and CAPA after approval.
Official Technical and Regulatory References
- U.S. FDA: Orthopedic Non-Spinal Bone Plates, Screws, and Washers - 510(k) Submission Guidance
- U.S. FDA: Fracture Fixation Plate Performance Criteria Guidance
- U.S. FDA: Quality Management System Regulation (QMSR)
- ISO: ISO 19227:2018 Cleanliness of Orthopedic Implants
- ASTM International: ASTM F136 Ti-6Al-4V ELI Surgical Implant Alloy
- ISO: ISO 11607-1 Packaging for Terminally Sterilized Medical Devices
- EUR-Lex: Regulation (EU) 2017/745 on Medical Devices

